
Attracting European Retail Chains: Why to Partner with CE Certified USB Extension Lead Manufacturers - Heikki Technology
The answer lies in establishing reliable partnerships with a verified Certified USB Extension Lead Manufacturer. Modern power strips have evolved from simple passive electrical outlets into multifunctional power hubs equipped with integrated USB charging ports, surge protection mechanisms, and intelligent power management microprocessors. For European retail buyers, securing inventory that carries full CE certification is not merely a legal requirement—it serves as the foundational safeguard for brand reputation, customer satisfaction, and long-term shelf stability.
European market regulations enforce strict health, safety, and environmental standards. Sourcing power extensions without authentic CE certification exposes importers and retail chains to significant supply chain vulnerabilities. By partnering with experienced manufacturing partners such as Heikki, European retail operators gain access to scalable production capabilities, stringent quality assurance protocols, and engineered electrical products tailored to regional demands.
Operational Challenges Facing European Retail Chains in Power Electronics
Managing consumer electronics and power distribution hardware across European retail networks requires navigating complex commercial and regulatory demands. Retail procurement managers face key operational pain points that directly affect gross margins and brand integrity.
1.Navigating Strict Regulatory Compliance and Certification Audit Risks
The European Union enforces rigorous electrical safety directives, including the Low Voltage Directive (LVD 2014/35/EU), the Electromagnetic Compatibility Directive (EMC 2014/30/EU), and the Restriction of Hazardous Substances Directive (RoHS 2011/65/EU). Customs authorities routinely inspect incoming shipments for valid CE documentation, test reports, and compliance certificates. Non-compliant electrical imports risk immediate seizure, heavy financial fines, and mandatory market withdrawal, resulting in empty retail shelves and substantial lost revenue.
2.Mitigating High Product Return Rates and Customer Dissatisfaction
Power strips and USB extension leads are high-frequency household appliances. Subpar interior copper wiring, fragile casing materials, or unstable transformer modules in uncertified USB chargers lead to overheating, erratic charging speeds, and short circuits. High return rates destroy product margins and damage the consumer trust that retail chains spend years establishing.
3.Minimizing Inventory Stagnation and Supply Chain Bottlenecks
Retail supply chains require predictable manufacturing schedules and consistent product quality. Unreliable OEMs with inconsistent output or unverified component suppliers frequently cause delivery delays. Furthermore, stocking generic, poorly designed power boards leads to slow inventory turnover, forcing retailers to mark down unverified stock.
The Role of Authentic CE Certification in Resolving European Retail Challenges
Authentic CE certification serves as a direct technical and operational remedy to the core vulnerabilities troubling European retail supply chains. By establishing strict engineering benchmarks for USB extension leads, valid certification systematically resolves each operational bottleneck facing retail procurement.
Solution 1 - Eliminating Regulatory Risks Through Factory-Backed Technical Files
To counteract customs blockades and compliance penalties, authentic CE certification requires comprehensive testing under LVD and EMC directives. Partnering with a manufacturer that maintains verified certification guarantees that every shipment is backed by valid Technical Construction Files (TCF) and official Declarations of Conformity (DoC). This documentation enables frictionless customs clearance across all EU member states, insulating retail chains from regulatory fines and stock confiscation.
Solution 2 - Neutralizing Quality-Driven Product Returns with Rigorous Safety Testing
CE compliance directly targets high return rates by mandating strict dielectric strength, thermal resistance, and electromagnetic stability tests. Products must withstand high insulation resistance testing to eliminate electric shock hazards, utilize fire-retardant thermoplastics to prevent thermal melting, and incorporate voltage regulation microprocessors within the USB module to deliver stable charging without overheating. These engineering standards prevent premature component failure, drastically reducing customer returns and protecting retailer margin integrity.
Solution 3 - Safeguarding Inventory Velocity and Supply Chain Stability
Authentic CE certification functions as a quality filter that eliminates production inconsistencies. Working with a certified manufacturer ensures that standardized raw materials, automated soldering processes, and strict batch-level testing protocols are applied to every production run. This consistency prevents shipment rejections, eliminates localized safety recalls, and delivers high-performing electrical goods that command steady sell-through rates, protecting retailers against inventory stagnation.
Core Technical Competencies and Architectural Excellence in Modern Power Strips
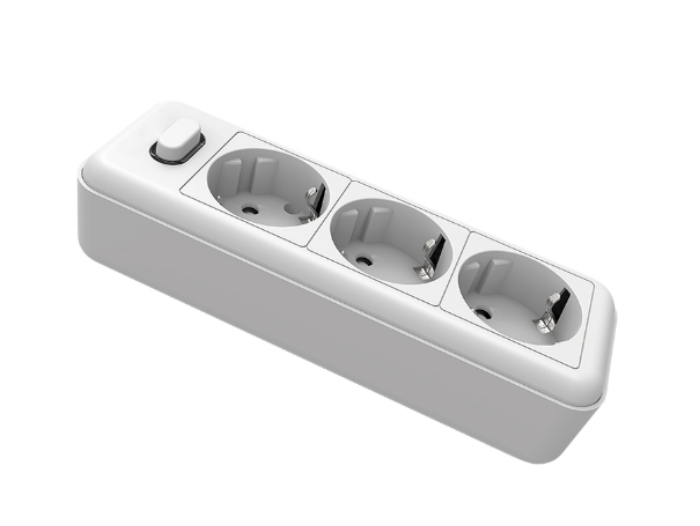
To understand why direct factory partnerships offer superior value to European retailers, it is necessary to examine the structural engineering and manufacturing standards required for certified power distribution products. A representative benchmark in this category is the EU CE Certified Power Board 5 AC Socket Extension Socket with 10A Rated Current.
Heavy-Duty Structural Enclosures and Flame-Retardant Thermoplastics
Commercial-grade power strips utilize high-impact, fire-retardant enclosures. Materials are subjected to glow-wire testing at elevated temperatures (such as 750°C or 850°C) to ensure self-extinguishing properties, minimizing fire risks in home and office environments.
Optimized Integrated Copper Bar Architecture
Conventional low-cost power strips rely on individual wire leads soldered between socket contacts—a design prone to cold solder joints, higher internal resistance, and premature failure. Premium manufacturing employs an integrated pure copper strip construction. Stamped from high-conductivity brass or phosphor bronze, this continuous conductor architecture lowers electrical resistance, minimizes heat accumulation during continuous 10A load operations, and maintains structural elasticity over thousands of insertion cycles.
Advanced USB Charging Electronics and Circuit Protection
Modern USB extension leads integrate dedicated PCBA modules offering multiple USB-A and USB-Type-C ports. Advanced models incorporate smart IC chips that automatically detect connected devices, optimizing power delivery while providing multi-stage protection against over-voltage, over-current, short circuits, and elevated operating temperatures.
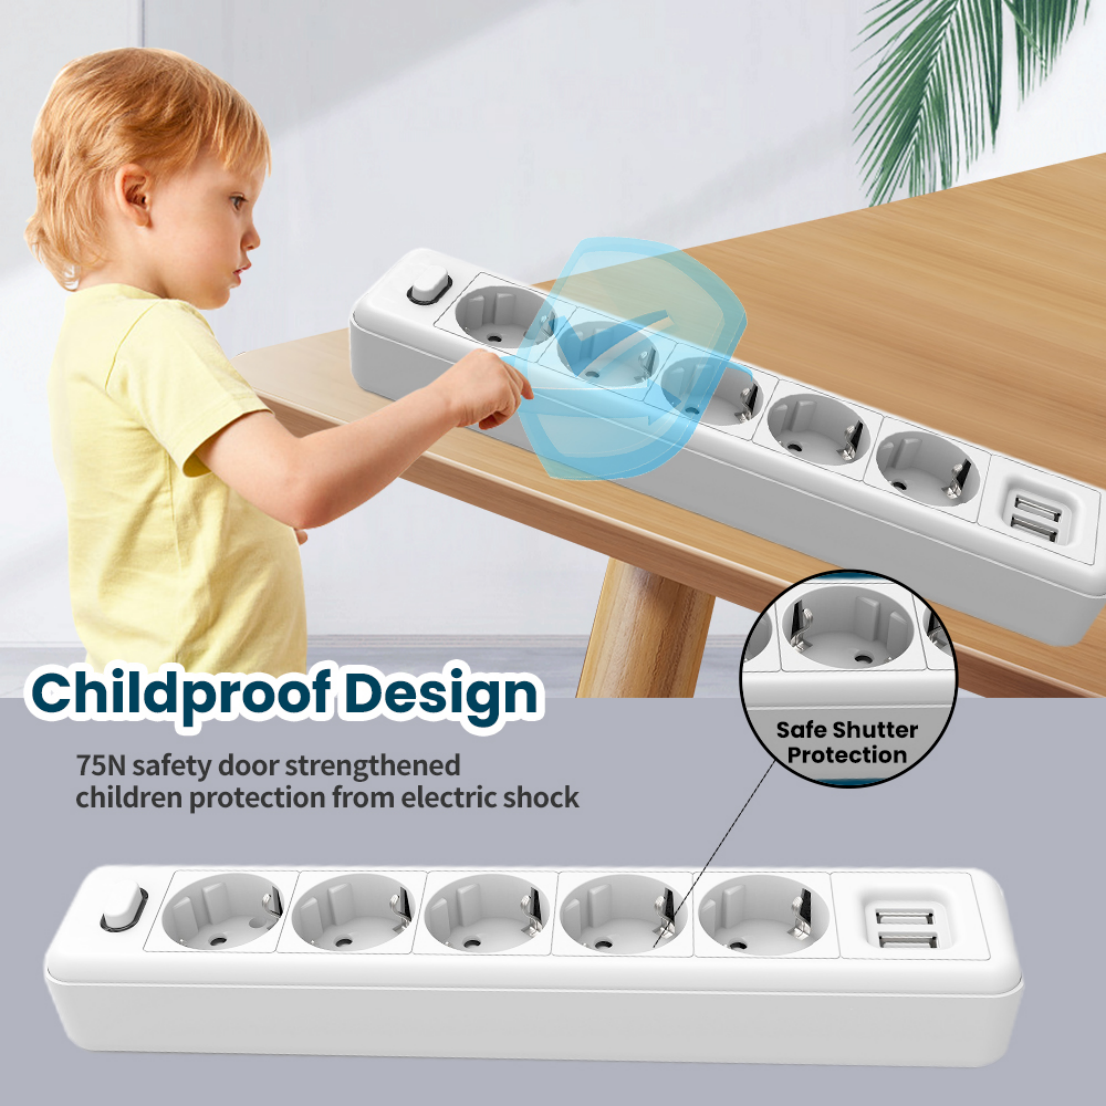
Safety Shutters and Ergonomic Child Protection
European home safety standards require integrated child-proof safety shutters within each AC socket. Internal mechanical barriers prevent the insertion of foreign objects into live contacts, requiring equal simultaneous pressure on both live and neutral apertures to open.
Key Operational Advantages of Partnering with Heikki Technology
Navigating the global manufacturing landscape requires identifying production partners equipped with technical depth, extensive facilities, and documented quality compliance. Heikki Technology represents a fully integrated manufacturing platform structured to fulfill the volume and quality needs of multinational retail chains.
Over Three Decades of Manufacturing Leadership and Industrial Infrastructure
Operating a self-owned manufacturing campus covering more than 30,000 square meters in Jianghai District, Jiangmen, Guangdong, the enterprise brings over 30 years of specialized manufacturing experience in power strips and electrical adapters. Recognized with "Specialized, Refined, Unique, and Innovative SMEs" and "High and New-Technology Enterprise (HNTE)" designations, the company maintains continuous production capacity alongside full-cycle R&D, structural design, tooling development, and international sales operations.
Comprehensive International Quality Systems and Global Approvals
Quality management is grounded in ISO 9001 (Quality Management), ISO 14001 (Environmental Management), and ISO 45001 (Occupational Health and Safety) certifications. Beyond European CE and UKCA approvals, the manufacturer maintains global safety certifications across diverse regional markets—including GCC (Middle East), SQM (Saudi Arabia), ESMA (Dubai), BS1363 (Hong Kong), SS145 (Singapore), MS589 (Malaysia), PS (Philippines), KC (South Korea), TISI (Thailand), SON (Nigeria), CB schemes, and CCC. This global certification footprint demonstrates a deep mastery of electrical engineering regulations.
Complete OEM/ODM Customization for Private Label Retailers
Retail chains require tailored product offerings to differentiate their store brands. The factory provides comprehensive OEM/ODM solutions, supporting custom housing colors, tailored cable lengths, regional plug variations (EU Type C/F, UK BS1363, French Type E), specialized retail packaging, and laser-engraved branding.
Strategic Procurement Alignment: Building Resilient European Retail Supply Chains
For European retail buyers, wholesale importers, and brand distributors, selecting a power hardware supplier is a long-term strategic decision. The combination of verified compliance, advanced product engineering, and high-volume manufacturing capabilities enables retail chains to optimize inventory performance and expand market share.
By partnering with an established certified manufacturer, retail buyers can:
Eliminate regulatory risks through factory-backed documentation and authentic CE, UKCA, and RoHS certifications.
Enhance retail profit margins by dealing directly with a fully integrated production facility, eliminating unnecessary intermediary costs.
Ensure consistent shelf availability through automated production lines, rigorous aging tests, and standardized quality control.
Offer modern, user-friendly designs that feature fast USB charging, child safety shutters, and durable flame-retardant construction.
Building a dependable product catalog in consumer electronics relies on foundational manufacturing excellence. Partnering with a proven OEM/ODM manufacturer allows European retail networks to deliver reliable, safe, and certified power extension solutions to consumers while maintaining supply chain stability.
For detailed technical specifications, product catalog inquiries, and global OEM/ODM collaboration opportunities, visit the official corporate portal: https://www.heikkitech.com/
Jiangmen Heikki Technology CO.,Ltd
Jiangmen Heikki Technology CO.,Ltd
email us here
Legal Disclaimer:
EIN Presswire provides this news content "as is" without warranty of any kind. We do not accept any responsibility or liability for the accuracy, content, images, videos, licenses, completeness, legality, or reliability of the information contained in this article. If you have any complaints or copyright issues related to this article, kindly contact the author above.
